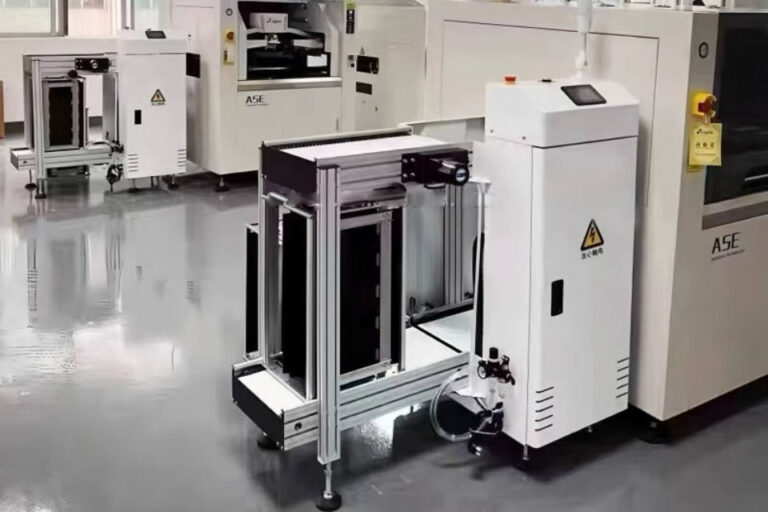
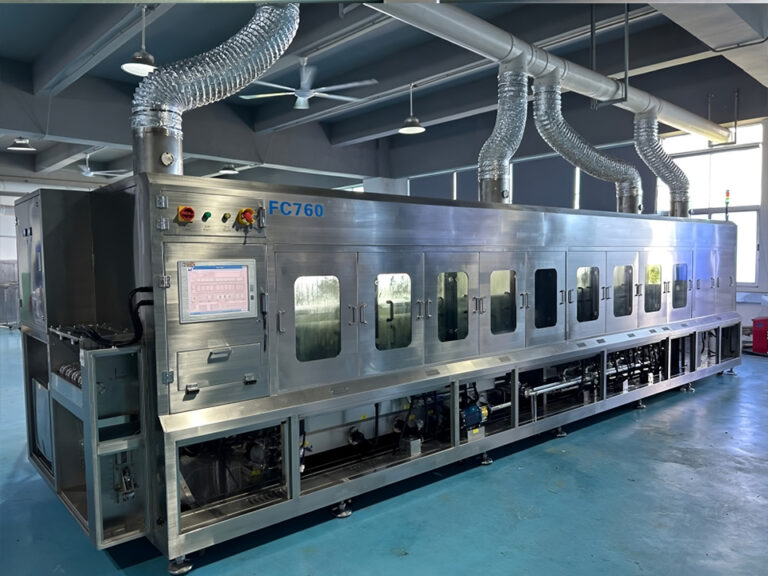
When I model a greenfield electronics plant, I start with takt time, positionings per board, transition losses, evaluation escapes, feeder availability, and upkeep insurance coverage, due to the fact that a shiny “lights-out” layout can take in millions while still missing out on deliveries.
Why automate a still procedure?
The honest solution is that most new manufacturing facilities require discerning SMT automation, not optimal automation. Automate solder-paste printing, component positioning, reflow, and examination initially. Maintain low-frequency product activity, remodel, odd-form insertion, and some board dealing with handbook until manufacturing information validates the following investment.
That seems conservative. It is.
However over-automation is one of the electronic devices market’s extra costly vanity tasks: the manufacturing facility purchases conveyor areas, robot loaders, smart storage, and software assimilations prior to it has steady products, educated service technicians, or enough need to keep one shift busy.
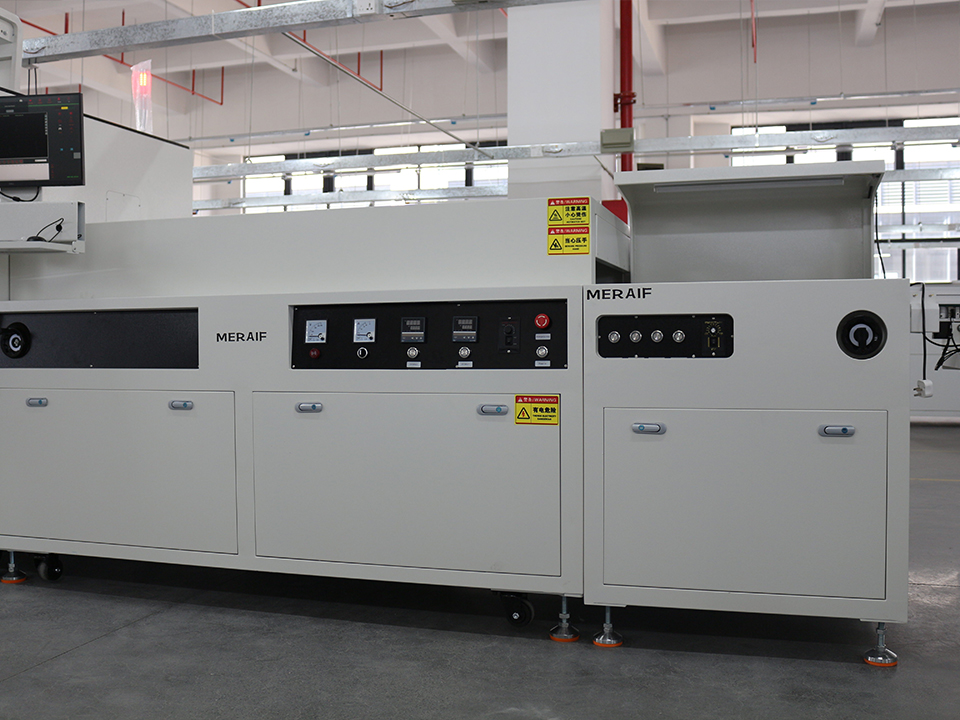
The Short Response: Most Brand-new Manufacturing Facilities Required Degree 2 or Level 3 SMT Automation
I make use of a five-level planning scale:
- Level 1– Core maker automation: Automated printing, pick-and-place, and reflow, with hand-operated loading, evaluation, and material motion.
- Degree 2– Inline SMT automation: Loader, printer, SPI, positioning machines, reflow oven, AOI, conveyors, and unloader attached as one line.
- Level 3– Data-connected automation: Degree 2 plus barcode traceability, feeder verification, product control, dish administration, control panels, and MES combination.
- Level 4– Autonomous intralogistics: Automated storage, reel retrieval, mobile robots, predictive replenishment, and minimal driver treatment.
- Level 5– Lights-out production: Automated organizing, material circulation, changeovers, examination transmitting, and exception handling across several lines.
For a new factory, Level 2 is generally the practical beginning factor. Level 3 becomes warranted when clients call for serial-number traceability, regulated documents, element ancestry, or fast root-cause analysis.
Degree 4 makes good sense only when numerous lines share materials and operate throughout two or three shifts. Level 5 is hardly ever a sensible starting point.
Below is my candid rule: if management can not state anticipated month-to-month board quantity, placements per board, changeovers per shift, target first-pass yield, and offered maintenance reaction time, administration is not ready to accept full SMT line automation.
Start With Placement Mathematics, Not Machine Catalogs
Begin with need.
A supplier might market 80,000 elements per hour, yet that number can fall down under genuine production conditions involving 01005 components, 0.4 mm-pitch BGAs, vision examination, feeder travel, nozzle changes, board warpage, and blended placement elevations.
What does the manufacturing facility actually require?
Use this preparation equation:
Called for nominal CPH = Daily boards × placements per board ÷ set up hours ÷ OEE ÷ product-efficiency aspect
Expect the manufacturing facility anticipates:
- 1,200 boards per day
- 850 placements per board
- Two eight-hour shifts
- 65% overall equipment performance
- 75% product-efficiency variable
The computation is:
1,200 × 850 ÷ 16 ÷ 0.65 ÷ 0.75 = 130,769 CPH
Include 15% growth clearance, and the ideal small target becomes approximately 150,000 CPH.
Do not quit there. The printer, SPI, reflow oven, AOI, conveyors, and material-replenishment system have to sustain the exact same board rate. A 150,000-CPH positioning cell connected to a slow-moving AOI program is not a 150,000-CPH SMT production line.
It is inventory storage space with strobe lights.
Track five numbers prior to selecting SMT equipment:
- Boards per hour
- Placements per hour
- Transition minutes per product
- First-pass yield
- Unexpected downtime mins per change
And use real item households– not one ordinary board that exists only in a spread sheet.
Match the Automation Degree to the Factory Profile
The adhering to ranges are preparing assumptions, not supplier quotations. Devices brand name, positioning rate, feeder matter, assessment extent, regional assistance, import prices, and new-versus-used investing in can move the last figure significantly.
| Factory profile | Regular monthly output | Typical product mix | Recommended automation | Tools budget plan allowance * |
|---|---|---|---|---|
| Model and NPI | Under 10,000 boards | Very high mix, regular engineering changes | Degree 1: printer, adaptable placer, reflow, offline examination | $150,000–$600,000 |
| High-mix manufacturing | 10,000– 75,000 boards | 20– 100 energetic settings up | Level 2 with SPI, AOI, feeder verification, and offline configuration | $600,000–$2 million |
| Growth manufacturing facility | 75,000– 250,000 boards | Moderate mix, 1 or 2 shifts | Level 2– 3 with traceability, MES link, and automated handling | $1.5–$4 million |
| High-volume manufacturing facility | More than 250,000 boards | Stable products, long production runs | Level 3– 4 with replicate feeders, automated storage space, and repetitive examination | $3–$8 million or even more |
- Budgetary allowance for line equipment and sustaining assets; structure job, HEATING AND COOLING, compressed air, electrical upgrades, taxes, and financing are excluded.
I would certainly reserve an additional 15% to 30% for feeders, nozzles, carts, extra components, offline programming, installment, training, profiling tools, and initial procedure debugging. New buyers consistently budget for the visible machines and neglect the properties that maintain those equipments running.
A second tough truth: yearly quantity is a weak sizing statistics. Making 600,000 the same boards is less complicated to automate than generating 120,000 boards spread out throughout 80 assemblies with multiple component substitutions.
Changeovers take in ability. Variation takes in engineering time.
Feeder Method Can Matter Greater Than Positioning Rate
Feeding decides uptime.
A technically quick placement device becomes a costly conveyor whenever drivers are searching for reels, fixing ignored feeders, verifying alternative parts, or rebuilding configurations straight on the production line.
This is why I analyze the feeder community prior to comparing heading CPH.
A Panasonic procedure, as an example, should evaluate the availability, calibration, and interchangeability of a Panasonic CM and NPM high-precision feeder system prior to committing to a platform. A combined fleet may likewise call for a reputable resource for Panasonic NPM, CM402, and CM602 feeders so development does not delay since a quotation left out production-ready feeder amounts.
The exact same rule uses somewhere else. A factory taking into consideration an initial Hanwha SM471Plus pick-and-place equipment need to price feeders, nozzles, carts, software application licenses, and regional service alongside the machine itself.
For Fuji individuals, carts are not devices. They are changeover infrastructure. Standardizing arrangements around an original Fuji NXT feeder cart or an original Fuji XPF feeder cart can move configuration job offline and return manufacturing minutes to the line.
My recommended beginning stock is not “one feeder per energetic port.” That leaves no resilience. Develop the feeder matter from energetic slots, simultaneous offline setups, plan widths, maintenance rotation, common-component duplication, and expected item overlap.
Procedure changeover from the last excellent board of Product A to the very first excellent board of Product B. Anything less is accounting fiction.
Automate Quality Prior To Automating Every Transfer
Quality requirements layers.
For a commercial automatic PCB assembly line, I normally focus on these controls:
- Closed-loop pattern printing where procedure risk sustains it
- 3D solder-paste assessment for fine-pitch, BGA, LGA, QFN, and high-value assemblies
- Positioning confirmation and feeder-component recognition
- Managed reflow profiling
- Post-reflow AOI
- X-ray examination for covert solder joints
- Electric test or useful test
- Unit-level and component-lot traceability
SPI and AOI do various work. SPI actions transferred paste before elements and heat make complex the problem. AOI checks visible post-reflow conditions. Neither changes X-ray for concealed BGA joints, bottom-terminated components, or nullifying evaluation.
Chemistry changes the choice as well. SAC305 solder– Sn96.5/ Ag3.0/ Cu0.5– does not immediately call for nitrogen reflow. Nitrogen should be bought for a measurable wetting, oxidation, deposit, or process-window purpose, not due to the fact that a salesman put “N ₂ all set” in vibrant type.
And information collection is not immediately helpful. If the manufacturing facility records reel IDs, solder-paste whole lots, moisture-sensitive-device exposure, stove dishes, evaluation outcomes, and serial numbers yet can not obtain a total background within minutes, it has developed an information garbage dump.
So automate the responses loophole:
- Spot the defect.
- Identify the affected systems.
- Link it to product and process background.
- Deal with the procedure.
- Verify that the flaw price dropped.
That is meaningful electronic devices producing automation.
What 2023– 2024 Manufacturing Facility Information In Fact Informs Us
The automation wave is genuine. The International Federation of Robotics reported 4,281,585 industrial robotics running worldwide in 2023, a 10% rise, while typical production robotic thickness got to 162 robots per 10,000 employees.
However national robot density is not a prescription for an SMT line. It just confirms that automation is ending up being regular facilities. Reuters reported in November 2024 that South Korea had actually gotten to 1,012 robotics per 10,000 manufacturing workers, the greatest thickness determined in the IFR comparison.
High density does not imply every procedure must be automated. It implies factories have actually learned where automation pays.
Rivian deals the much more uncomfortable lesson. During its 2024 Illinois factory retooling, the firm eliminated more than 100 battery-production actions, gotten rid of 52 body-shop equipments, cut over 500 components, and reported a 30% improvement in production-line effectiveness. This was automotive production, not SMT, so I deal with the verdict as an operational reasoning: simplifying the process can produce more capacity than adding equipments.
NIST’s 2023 small-and-medium-manufacturer research took an in a similar way grounded method by checking automation at the task and procedure level with all 51 Production Expansion Partnership focuses. That is the appropriate device of evaluation. “How automatic is the factory?” is vague; “which task is producing labor, top quality, or throughput loss?” can be gauged.
The evidence supports a placement suppliers seldom advertise: even more automation is not immediately more productive.
The 4 Examinations Every Automation Purchase Should Pass
I approve an automation job only when it passes 4 tests.
1. The Capability Examination
Will the devices remove a measured bottleneck at projection need– not an optimistic sales projection?
Determine the expense per good board at 40%, 60%, and 80% application. If the investment works only at 90%, business situation is fragile.
2. The Quality Test
Will it protect against, identify, or include an issue that has a significant economic or consumer impact?
Automated assessment is less complicated to safeguard when one left problem can trigger field service, containment, delivery hold-ups, or an item recall.
3. The Labor Test
Does automation eliminate repeated handling, or does it just change one operator with a developer, maintenance specialist, material specialist, and software application manager?
Automation changes labor. It hardly ever makes labor go away.
4. The Versatility Examination
Can the system deal with brand-new PCB measurements, heavier boards, element substitutions, tray-fed components, weird bundles, much shorter sets, and client traceability demands?
A fast maker that can not take in product change is not adaptable capability. It is a set wager.
Usual SMT Automation Errors
The worst mistakes appear practical throughout acquiring conferences:
- Purchasing positioning rate before calculating changeover losses
- Treating advertised CPH as sustainable CPH
- Purchasing as well couple of feeders and carts
- Automating conveyors while material replenishment continues to be chaotic
- Adding MES prior to defining trusted information ownership
- Utilizing AOI as a replacement for procedure control
- Disregarding professional training and spare-parts preparation
- Building one large line when two smaller sized lines would offer far better redundancy
- Automating unpredictable products prior to design-for-manufacturing problems are corrected
- Presuming “totally automatic” means unattended
The final point is worthy of focus. A line can fill, print, check, place, reflow, check once more, and dump immediately while still depending upon people for reel replenishment, splice recognition, nozzle upkeep, stencil cleansing, paste control, program confirmation, alarm healing, and issue disposition.
The tag exists.
Regularly Asked Questions
Just how much SMT automation does a new electronics factory require?
The majority of brand-new electronics manufacturing facilities require careful SMT automation: automated solder-paste printing, pick-and-place, managed reflow, and AOI, while board loading, unloading, material movement, replenishment, revamp, and through-hole setting up stay hands-on till throughput, flaw expense, or labor information shows that another automated station will repay its resources and integration problem.
For many greenfield operations, that means Degree 2 automation at first, with the electric, floor-space, software, and conveyor stipulations needed for Level 3 later on.
Exactly how do I calculate the required SMT production-line capacity?
Compute needed SMT capacity by splitting day-to-day part positionings by scheduled production hours, after that separating once more by expected OEE and product-efficiency elements; add 10% to 20% growth headroom, and confirm that printing, reflow, AOI, feeder transition, maintenance, and product replenishment can sustain the resulting board price.
Run different estimations for each and every significant item family. A simple board with 1,000 placements may run faster than a hard board with 400 positionings.
Is a fully automated SMT line best for a brand-new factory?
A totally automated SMT line is best just when demand is steady, product designs are fully grown, change insurance coverage is sufficient, product circulation is disciplined, and the forecasted cost savings from dealing with, traceability, quality control, and throughput go beyond the consolidated costs of tools, assimilation, upkeep, software, saves, training, and operational intricacy.
If need doubts, develop a modular line. Protect development space, standard interfaces, extra electrical capability, network decreases, exhaust ability, and a path for conveyors or inspection stations.
What is the most effective SMT automation for a new factory?
The most effective SMT automation for a brand-new factory is a modular Degree 2 line containing an automatic printer, SPI where issue risk warrants it, adaptable pick-and-place capability, regulated reflow, AOI, board conveyors, and offline feeder prep work, supported by equipment vendors that can provide training, software, feeders, spares, and local technological service.
Brand loyalty should come after service protection, feeder economics, real-product trials, software application compatibility, and total price per great board.
When should a factory add SPI and AOI?
A manufacturing facility should add SPI when solder-paste variant can produce pricey defects and include AOI when visible post-reflow mistakes need regular detection, particularly for fine-pitch tools, high element counts, high-value boards, regulated items, multiple changes, or production volumes that make hands-on assessment slow, irregular, and hard to document.
For BGAs and other hidden joints, include an X-ray technique. AOI can not check what its electronic cameras can not see.
Just how much extra spending plan should be scheduled beyond the major SMT machines?
A brand-new manufacturing facility needs to usually schedule 15% to 30% beyond the heading machine costs for feeders, carts, nozzles, spare parts, shows tools, installation, products, training, process recognition, utilities, traceability combination, profiling devices, and early-production assistance, with a larger reserve when tools is imported or regional solution coverage is weak.
Likewise model functioning funding for component inventory, solder paste, patterns, moisture-control equipment, assessment programming, and certification develops.
Develop the Line Around Your Products
Do not ask a provider for a “fully automated SMT line” and wait on a shopping list.
Bring the product information: Gerber files, BOMs, centroid documents, panel measurements, element bundles, positionings per board, target volumes, batch dimensions, changeover frequency, top quality requirements, change strategy, and three-year need scenarios.
After that call for a line-capacity design, feeder routine, bottleneck evaluation, staffing plan, energy strategy, acceptance examination, spare-parts list, and growth course.
That is how to automate an SMT production line without getting a monument to a positive forecast.
All set to define your factory? Request an SMT line review based upon your real item mix, throughput target, feeder requirements, examination danger, and expansion strategy– and spend only where the numbers sustain it.