Yes, one SMT line can produce both lead-free and leaded settings up. Whether it must is a harder inquiry.
Segregation precedes.
On a common line, the actual control issue is not whether the printer, positioning machine, and oven can refine both alloys; it is whether materials, tooling, dishes, inspection limits, records, and human choices continue to be unmistakably divided through every transition.
Can one mislabeled solder-paste container concession an entire RoHS build?
Definitely.
I concern mixed solder setting up as a traceability problem disguised as a devices problem. Managers often tend to concentrate on stove ability because reflow temperature level shows up. Yet the more typical threats rest upstream and off-line: shared squeegees, inaccurately returned paste, unrestrained rework irons, partially utilized part reels, and boards waiting without clear standing recognition.
The tough fact is straightforward: a shared line conserves capital expenditure by producing a continuous process-control financial debt. If administration is unwilling to pay that debt through disciplined procedures, verification, training, and document retention, it needs to get or book a separate line.
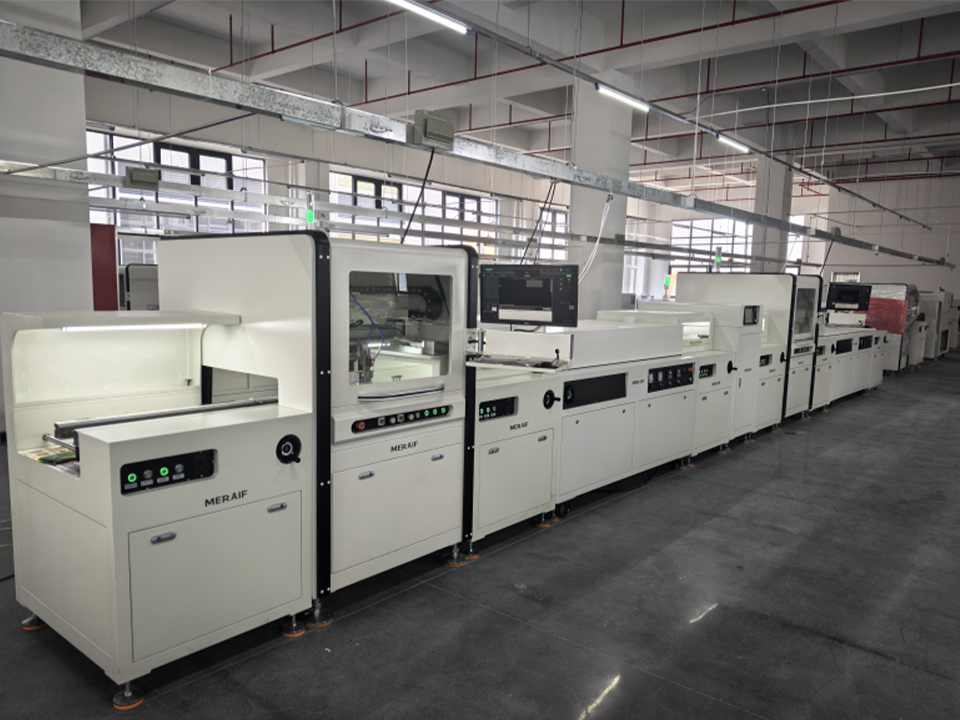
Can Lead-Free and Leaded Assemblies Share an SMT Line?
They can, gave the factory treats them as 2 individually regulated processes that occur to utilize several of the same machines.
Requirement eutectic Sn63Pb37 solder melts at around 183 ° C. SAC305– Sn96.5 Ag3.0 Cu0.5– generally thaws throughout about 217– 220 ° C. That difference influences the solder paste, stencil actions, change chemistry, thermal profile, part temperature direct exposure, inspection requirements, and rework settings.
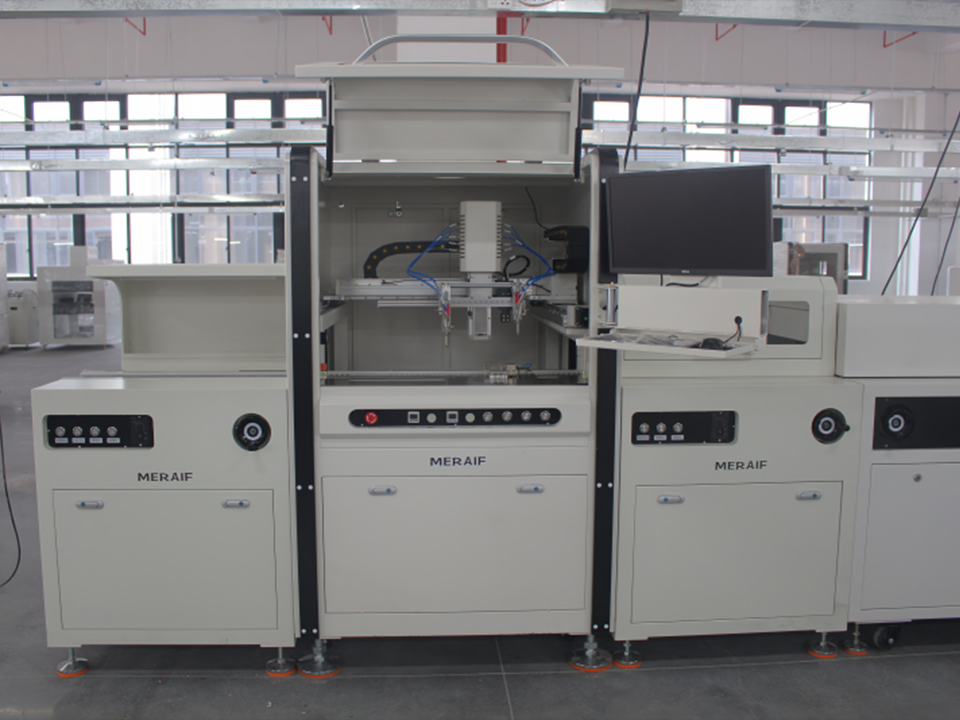
The common tools is rarely the determining factor. A programmable Panasonic NPM-GH positioning platform can position parts for either process since placement itself does not melt solder. The risk is packing the incorrect component coating, reel, feeder arrangement, or program against the work order.
A reflow oven might additionally run both procedures when it can replicate independently validated dishes. However certification must be board-specific. “Lead-free mode” is not a profile, and copying zone temperatures from one more item is not recognition.
My preferred operating policy is:
- Run lead-free production from a validated clean state.
- Set up tin-lead production later when useful.
- Carry out the full confirmed changeover prior to going back to lead-free job.
- Never treat manufacturing series as a substitute for material controls.
- Use committed tooling anywhere solder paste or liquified alloy makes straight call.
Organizing decreases exposure. It does not prove compliance.
Why Cross-Contamination Occurs Where Managers Least Anticipate It
SMT line cross-contamination generally starts with ordinary items instead of amazing equipment failings.
The printer is the highest-risk shared machine due to the fact that paste touches the stencil, mops, understencil cleansing media, assistance tooling, spatulas, and waste containers. A trace of SnPb paste brought right into a lead-free job can produce a local lead focus much past the nominal 0.1% homogeneous-material limitation applied to lead under RoHS guidelines.
Revamp is even worse.
A specialist can use the incorrect solder cable, idea, flux pen, pigtail, or hot-air account in secs. The fixed board may then pass useful testing since electrical feature does not develop chemical compliance.
The main transfer and replacement paths are:
- Solder-paste containers returned to the wrong refrigerator area
- Shared patterns or mops without verified cleansing
- Paste residue on printer tooling and taking care of applies
- Inaccurate reels or moisture-sensitive tools released to a job
- Shared soldering tips, wire, braid, flux, and solder pots
- Combined WIP at examination, repair work, or barrier terminals
- Wrong reflow dish picked after a product change
- Scrap or quarantined boards reestablished without permission
- Leaded labels eliminated before final packaging
- Agreement assemblers accepting undocumented part replacements
Color coding assists, however shade is not a control system. Use barcode identity at product concern, equipment loading, recipe selection, remodel, and last launch. The checked product number must be checked versus the approved BOM and procedure path– not simply videotaped after the truth.
Regulatory Evidence Says the Exemption Must Adhere To the Item
RoHS compliance belongs to the ended up item and its uniform products, not to the manufacturing facility’s recommended advertising label.
European Commission assistance states that RoHS exceptions are time-limited, reflected on, and assessed against replacement accessibility, integrity, health and wellness, ecological, socioeconomic, and advancement factors. Revival applications typically should be filed at the very least 18 months prior to expiration.
A 2023 European Payment influence evaluation noted that lead solders in electrical and digital tools have actually been outlawed since 2006, based on exceptions that considerably run out and are not constantly restored. That need to finish the lazy assumption that an exception used for last year’s construct continues to be legitimate forever.
The auto policies reveal why transmitting should be product-specific. Payment Delegated Regulation (EU) 2023/544 retained lead-solder arrangements for specified tradition applications, consisting of circuit-board settings up for lorries type-approved prior to January 1, 2016, and their spare parts. That is an End-of-Life Cars exception, not bury approval to label unrelated electronic devices certified.
British federal government assistance likewise specifies a 0.1% optimum lead concentration in applicable homogeneous materials, subject to exclusions and exemptions. It also needs supporting technological paperwork and ten-year supply-chain traceability for protected economic drivers.
So the tourist needs to identify:
- Market and controling guideline
- Item classification
- Customer solder demand
- Accepted alloy and paste part number
- Component-finish demands
- Appropriate exemption and expiration standing
- Verified printer and reflow programs
- Assessment plan
- Rework alloy and device family members
- Called for certifications and retention duration
A tourist noted only “RoHS” or “non-RoHS” is precariously slim.
Construct a Physical and Digital Partition System
Separate anything that directly get in touches with solder alloy. Control whatever that can transform product identity.
That difference matters due to the fact that factories in some cases devote expensive feeders while allowing one paste spatula to roam between workbenches. The cash mosts likely to the incorrect danger.
| Control factor | Lead-free production | Leaded manufacturing | Required proof |
|---|---|---|---|
| Solder paste | Secured, identified SAC305 or approved alloy | Locked Sn63Pb37 or approved SnPb alloy | Whole lot, expiration, thaw time, problem and return checks |
| Stencil and mops | Dedicated or validated-clean LF set | Devoted or validated-clean PB collection | Tool ID and cleaning document |
| Impressora | Approved LF program and clean-state release | Accepted SnPb program | Changeover checklist and first-print authorization |
| Elements | Approved coatings and BOM alteration | Approved heritage or exempted components | Reel-level check and provider affirmation |
| Positioning | Recipe locked to work order | Different regulated dish | Program checksum or modification document |
| Reflow | Board-specific lead-free profile | Board-specific tin-lead account | Dated thermal-profile record |
| Revamp | Dedicated iron, pointers, wire, braid, and change | Different marked device family members | Service technician and repair service background |
| Evaluation | LF handiwork library | SnPb handiwork library | SPI, AOI, X-ray, and disposition documents |
| Launch | RoHS evidence bundle | Client or exemption evidence | Serialized genealogy and sign-off |
Paste storage calls for more than a handwritten shelf label. Produce literally divided locations, distinctive container colors, restricted concern permissions, and electronic lot controls. Moisture-sensitive components should also continue to be under a logged storage space program; an ESD completely dry cabinet for PCB materials may sustain that program, however ESD defense alone does not develop wetness control. Verify relative-humidity efficiency, alarm systems, calibration, and gain access to history.
And do not forget waste. Utilized wipes, denied prints, paste containers, dross, and polluted cleaning media require clearly separated disposal streams.
Confirm 2 Reflow Processes, Not One Concession Recipe
A single “center” dish is generally bad engineering.
Common Sn63Pb37 settings up may come to a head around 205– 225 ° C, while SAC305 assemblies usually call for roughly 235– 250 ° C. These are working arrays, not global setpoints. The approved paste information sheet, part temperature level scores, board building and construction, thermal mass, and gauged joint temperature levels need to figure out the real process home window.
For each setting up, document:
- Ramp rate
- Preheat and soak habits
- Time above the alloy’s liquidus
- Peak temperature level at depictive joints
- Temperature level delta throughout the board
- Cooling down price
- Conveyor rate
- Area setups
- Profiling-board revision
- Thermocouple areas and accessory method
- Profile day, driver, and tools ID
A Suneast PCB reflow oven or one more multi-zone system may keep both recipes, yet accessibility needs to be linked to the checked work order. Operators should pass by between “Account 1” and “Profile 2” from memory.
Does a common reflow chamber instantly infect every lead-free board with lead? No. In many reflow operations, direct paste-contact surfaces and rework devices should have even more focus than the chamber itself. Still, change condensate, exhaust problem, board support equipment, and maintenance deposits call for a documented assessment.
Vacuum cleaner handling presents an additional choice point. If void reduction is needed for power tools, thermal pads, or bottom-terminated parts, examine vacuum cleaner reflow stove configurations versus both alloy households rather than assuming the same stress sequence will certainly create equal voiding and moistening.
Use SPI and AOI as Process Proof, Not Decorative Equipment
Assessment needs to detect the failing mode associated with the current chemistry.
Three-dimensional solder-paste examination can confirm deposit quantity, elevation, area, form, countered, and linking threat before components take in even more manufacturing worth. A Saki 3Si 3D SPI system for solder-paste inspection matters below, specifically when different program libraries and first-board authorization rules are developed for each procedure.
AOI after reflow ought to make use of alloy-appropriate approval criteria. Lead-free joints may show up duller or more granular than traditional SnPb joints; thoughtlessly applying a visual library tuned to glossy tin-lead fillets develops false phone calls while still missing real issues. A Saki 3Xi M110 3D AOI platform can sustain calculated inspection, however its dish, illumination, limits, part collection, and defect-disposition rules still require engineering possession.
SPI and AOI can not certify RoHS chemistry. They supply process proof.
Usage X-ray fluorescence screening when material confirmation is required, recognizing that geometry, plating density, calibration, detection limitations, and the definition of homogeneous material can make complex interpretation. Intensify skeptical outcomes to a certified laboratory approach instead of stating conformity from a hassle-free testing number.
Comply With a Transition Treatment That Can Survive an Audit
The most effective techniques for blended SMT production should suit a managed, signed process:
- Close the outbound job order and reconcile boards, paste, reels, and WIP.
- Eliminate and set apart the outward bound paste, stencil, mops, tools, and waste.
- Clean the printer, support tooling, conveyors, handling points, and determined contact surfaces.
- Inspect the clean state against the accepted visual or analytical standard.
- Check the incoming paste great deal, pattern, tooling, BOM, and program revision.
- Load the secured printer, placement, SPI, reflow, and AOI dishes.
- Validate element and MSL condition before positioning.
- Run a profiled or previously validated configuration board under the authorized policies.
- Evaluate the first post with SPI, AOI, X-ray, or lab checks as defined.
- Release manufacturing with independent sign-off and retain the resulting documents.
No quiet inconsistencies. If a driver finds the incorrect paste, an unidentified reel, or a board with unsure rework history, quit and quarantine the affected time home window. “It was probably fine” is not a personality.
NASA’s active JSC-66491 standard provides a valuable high-reliability benchmark: it needs a formal control-and-mitigation framework for efficiency and reliability dangers connected with lead-free tin modern technology in flight hardware and mission-essential devices. Your business factory may not run under NASA rules, however the control-plan state of mind deserves loaning.
Why This Self-control Matters Beyond One Manufacturing Lot
The 2024 Global E-waste Screen reported 62 billion kilograms of e-waste produced in 2022, while just 22.3% was officially accumulated and recycled. It additionally found that e-waste generation had expanded virtually five times faster than documented collection and recycling given that 2010.
That report also counted only 81 countries– 42% of those examined– with an e-waste plan, law, or regulation as of June 2023. Sixty-seven used expanded producer obligation.
Those numbers do not confirm that one blended line is eco substandard to two committed lines. They do show why product declarations, repairability, regulated substances, and end-of-life liability are approaching tighter examination.
My opinion is blunt: factories that can not rebuild a board’s paste great deal, element lots, process route, thermal dish, examination result, and remodel background ought to stop calling their production “traceable.” A folder of supplier PDFs is not genealogy.
Often Asked Questions
Can lead-free and leaded settings up work on the same SMT line?
Running lead-free and leaded settings up on one SMT line is a controlled mixed-production technique in which both solder systems share capital tools while dedicated materials, tooling, dishes, tags, cleansing actions, and launch documents stop lead transfer, recipe abuse, and loss of product-level conformity.
The method is practically viable, however it calls for verified changeovers, serialized traceability, different rework controls, and product-specific governing testimonial. Risky or contractually limited items may still need devoted equipment.
What is SMT line cross-contamination?
SMT line cross-contamination is the unintended transfer or misidentification of solder alloy, paste, parts, devices, deposits, or work-in-process that triggers a board’s real material make-up or recorded process path to differ from its approved BOM, consumer need, or regulatory affirmation.
The most revealed places are solder-paste printing, hand-operated rework, pattern cleansing, material storage space, WIP buffers, and repair work stations. Functional screening alone will certainly not disclose a chemical-compliance failing.
What is a lead-free reflow profile?
A lead-free reflow account is a gauged stove dish that controls board temperature in time for a defined alloy and assembly, usually accounting for SAC305’s about 217– 220 ° C melting variety, element temperature level limitations, time over liquidus, ramp price, saturate habits, optimal temperature level, and cooling down price.
Area setups alone are insufficient since different boards respond in a different way to the very same oven setups. Designers should profile real temperature levels at depictive low-mass and high-mass joints.
What makes a PCB setting up RoHS-compliant?
RoHS-compliant PCB assembly is an electronics manufacturing procedure that regulates limited substances in each homogeneous product, supports suitable exceptions with proof, and maintains technical paperwork, vendor affirmations, lot genealogy, and production documents so the producer can defend the consistency claim for the marketplace where the product is offered.
Lead-free paste does not immediately make the finished board compliant. Element surfaces, inner bundle materials, alternatives, repair work, finishes, cable televisions, and exception problems should additionally be reviewed.
Can one reflow stove procedure both solder alloys?
Making use of one reflow stove for both alloy families is an equipment-sharing choice that can be appropriate when each product has a verified thermal recipe, dish accessibility is locked, flux exhaust is kept, transitions are documented, and product-specific compliance is shown by product and process controls.
The stove has to duplicate both thermal windows without exceeding part scores. If careful or wave soldering is likewise existing, molten solder pots and nozzles need much more stringent alloy-separation controls than a standard reflow chamber.
Transform Mixed Manufacturing Into a Controlled Refine
Do not start with the concern, “Can our devices run both alloys?” Begin with, “Can our evidence show which process every board obtained?”
Map every contact factor, lock every recipe, commit risky tooling, profile both alloy households, and test the transition treatment with a willful mock mistake prior to releasing client production.
If your common line can not capture the incorrect paste, incorrect reel, wrong profile, or incorrect rework device before delivery, the procedure is not prepared. Request an SMT line and examination review to define the equipment, segregation controls, and recognition package your item mix in fact calls for.